When RTLS makes sense for material
Tag loads and packaging when a miss changes money during the shift. Continuous location only fits when the last scan is not already the truth.
What the material decision is
A real-time location system (RTLS) fills the minutes between events other systems already own. A barcode at the dock is true at the scan. A WMS putaway is true when someone confirms a bin. An MES complete is true at the station. An ERP transfer is true when stock moves on paper. None of those records follow a pallet, cage, or kit while it sits in the wrong buffer or rolls toward the wrong door.
That gap is asset tracking for material: location that stays current while the load moves between system events. For the layer definition, see what RTLS is. People decisions are covered in when RTLS makes sense for people. Forklift decisions are covered in when RTLS makes sense for forklifts. This page stays on pallets, cages, material, and packaging, and on whether WIP capital, delay impact, volume, and packaging make continuous location worth buying this quarter.
When WIP capital makes location pay
High work in progress (WIP) is often a trust problem dressed as a shortage problem. When cages and loads drift after the last MES or WMS event, planners protect the line by releasing more material than the process needs. Capital sits on the floor. Congestion grows. Live location lets the plant cut safety stock that existed only because nobody trusted where the last batch was. That is an inventory management and lean manufacturing decision as much as a search decision.
The case is strongest when the material on the floor is valuable, sequenced, or hard to replace, not when every carton is cheap and interchangeable. If a missing load can idle a cell for an hour, or if buffers already hold days of cost, medium-precision location around 1–3 m (3–10 ft) is usually enough to change release and dispatch. Coarse zone presence only answers which wing. Exact floor position is a different buy for dock-face or tight marks. Search and find with RTLS and production monitoring cover how that WIP trust problem shows up on the live hall.
When late or wrong loads cost real money
Some plants pay in fines, chargebacks, or stopped customer lines when the wrong pallet ships or the right one ships late. Automotive and other sequenced feeds make that pain sharp. A just-in-sequence or just-in-time miss is not a tidy warehouse variance. It is a contractual and production event.
RTLS helps when the expensive failure is a stale last scan or a lookalike cage pulled in error. Continuous location next to the shipment identity cuts those surprises. Industry practice for sequenced lines often tags the returnable carrier and keeps a digital load manifest on what that carrier holds, rather than a tag on every kit. Location does not replace ASN discipline or dock process. It closes the gap between the last scan and the trailer face. End-to-end patterns for that class of flow are in end-to-end JIT logistics visibility.
When delays have outsized impact
A five-minute search is cheap in a quiet spare-parts bay. The same five minutes on a bottleneck cell, a paint exit, or a dock window that closes with the trailer is expensive. Delay impact is the multiplier: how many people, machines, or customer commitments wait when one load is in the wrong place.
If waiting at a bottleneck costs more than walking the packaging area twice a shift, location can pay even before anyone talks about fleet size. If the hall is small, every truck is visible from dispatch, and a miss only means a short walk, the same technology is a poor buy. Match the spend to the cost of delay, not to hall area alone. Radio and accuracy choice still follow the decision in start with the decision, not the technology.
Volume and packaging change the tag math
Volume decides whether a miss is a rare annoyance or a daily drain. Low move counts can absorb walks and radio hunts. High move counts turn the same friction into overtime, extra trucks, and chronic buffer bloat. The plant that moves hundreds of unit loads per shift has a different return than the plant that moves a handful of expensive tools.
Packaging decides what you can tag without exploding total cost of ownership. Returnable packaging such as racks, stillages, cages, and reusable totes amortizes a durable tag across many trips. Lost returnables are themselves a cost case. One-way packaging such as cartons is a poor host for expensive hardware. Those loads usually ride shipment labels and dock events, or a tagged pallet or vehicle, rather than a tag glued to every expendable wall. Mixing those models without a clear host is how tag counts and battery rounds quietly kill the project. Whether the first tag class should be the mover or the load is covered in tagging the mover vs tagging the material.
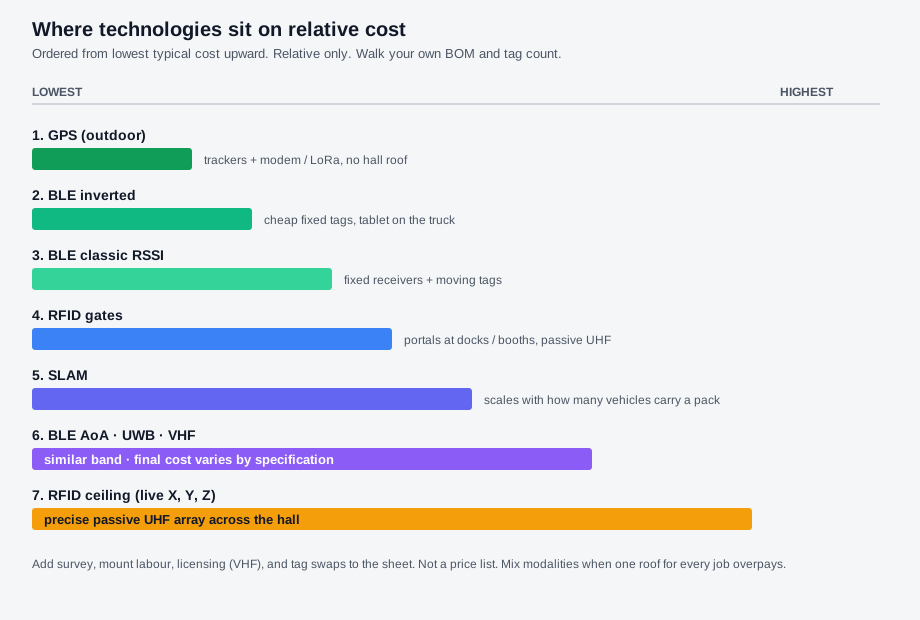
Different mixes, different ROI
High WIP capital plus returnable cages on a sequenced line is one case: tag the returnables, cut buffer stock, protect sequence. High volume of cheap one-way cartons with low delay cost is another: often skip load-level RTLS and keep ERP or WMS truth, as in live 3D stock from ERP without RTLS. High fines for wrong outbound plus moderate volume may justify dock-face and staging location without tagging every SKU in the hall.
Fleet empty miles and driver load are real benefits too, but they are separate use cases in internal logistics optimization and pinpointing non-value-added travel. Do not force one ROI story onto every plant. Name the money at risk, the packaging host, and the volume, then pick the use case that matches. Benefit jobs that share the same location layer are listed in where RTLS benefits show up. What to put in the cost model is in what to include when calculating RTLS ROI.
When you should skip
Skip when the last scan is already the truth the process will act on, and a miss is cheap. Skip when delay impact is low, WIP is light, and volume does not punish walking. Skip tagging every one-way carton for continuous location. Skip a hall-wide grid when a dock gate answers the only question that costs money. Skip the buy when nobody will own tags, batteries, and the map during the shift. Change management is part of the system. ROI does not show up from a dashboard nobody opens.
If the real fight is material call-offs nobody answers, that is material order automation, not locators on the ceiling. Once the economics say yes, capability depth for the live hall is on the features overview.
Get in touch if you want to walk the same cost mix (WIP, delay risk, volume, and packaging) on your own facility model.